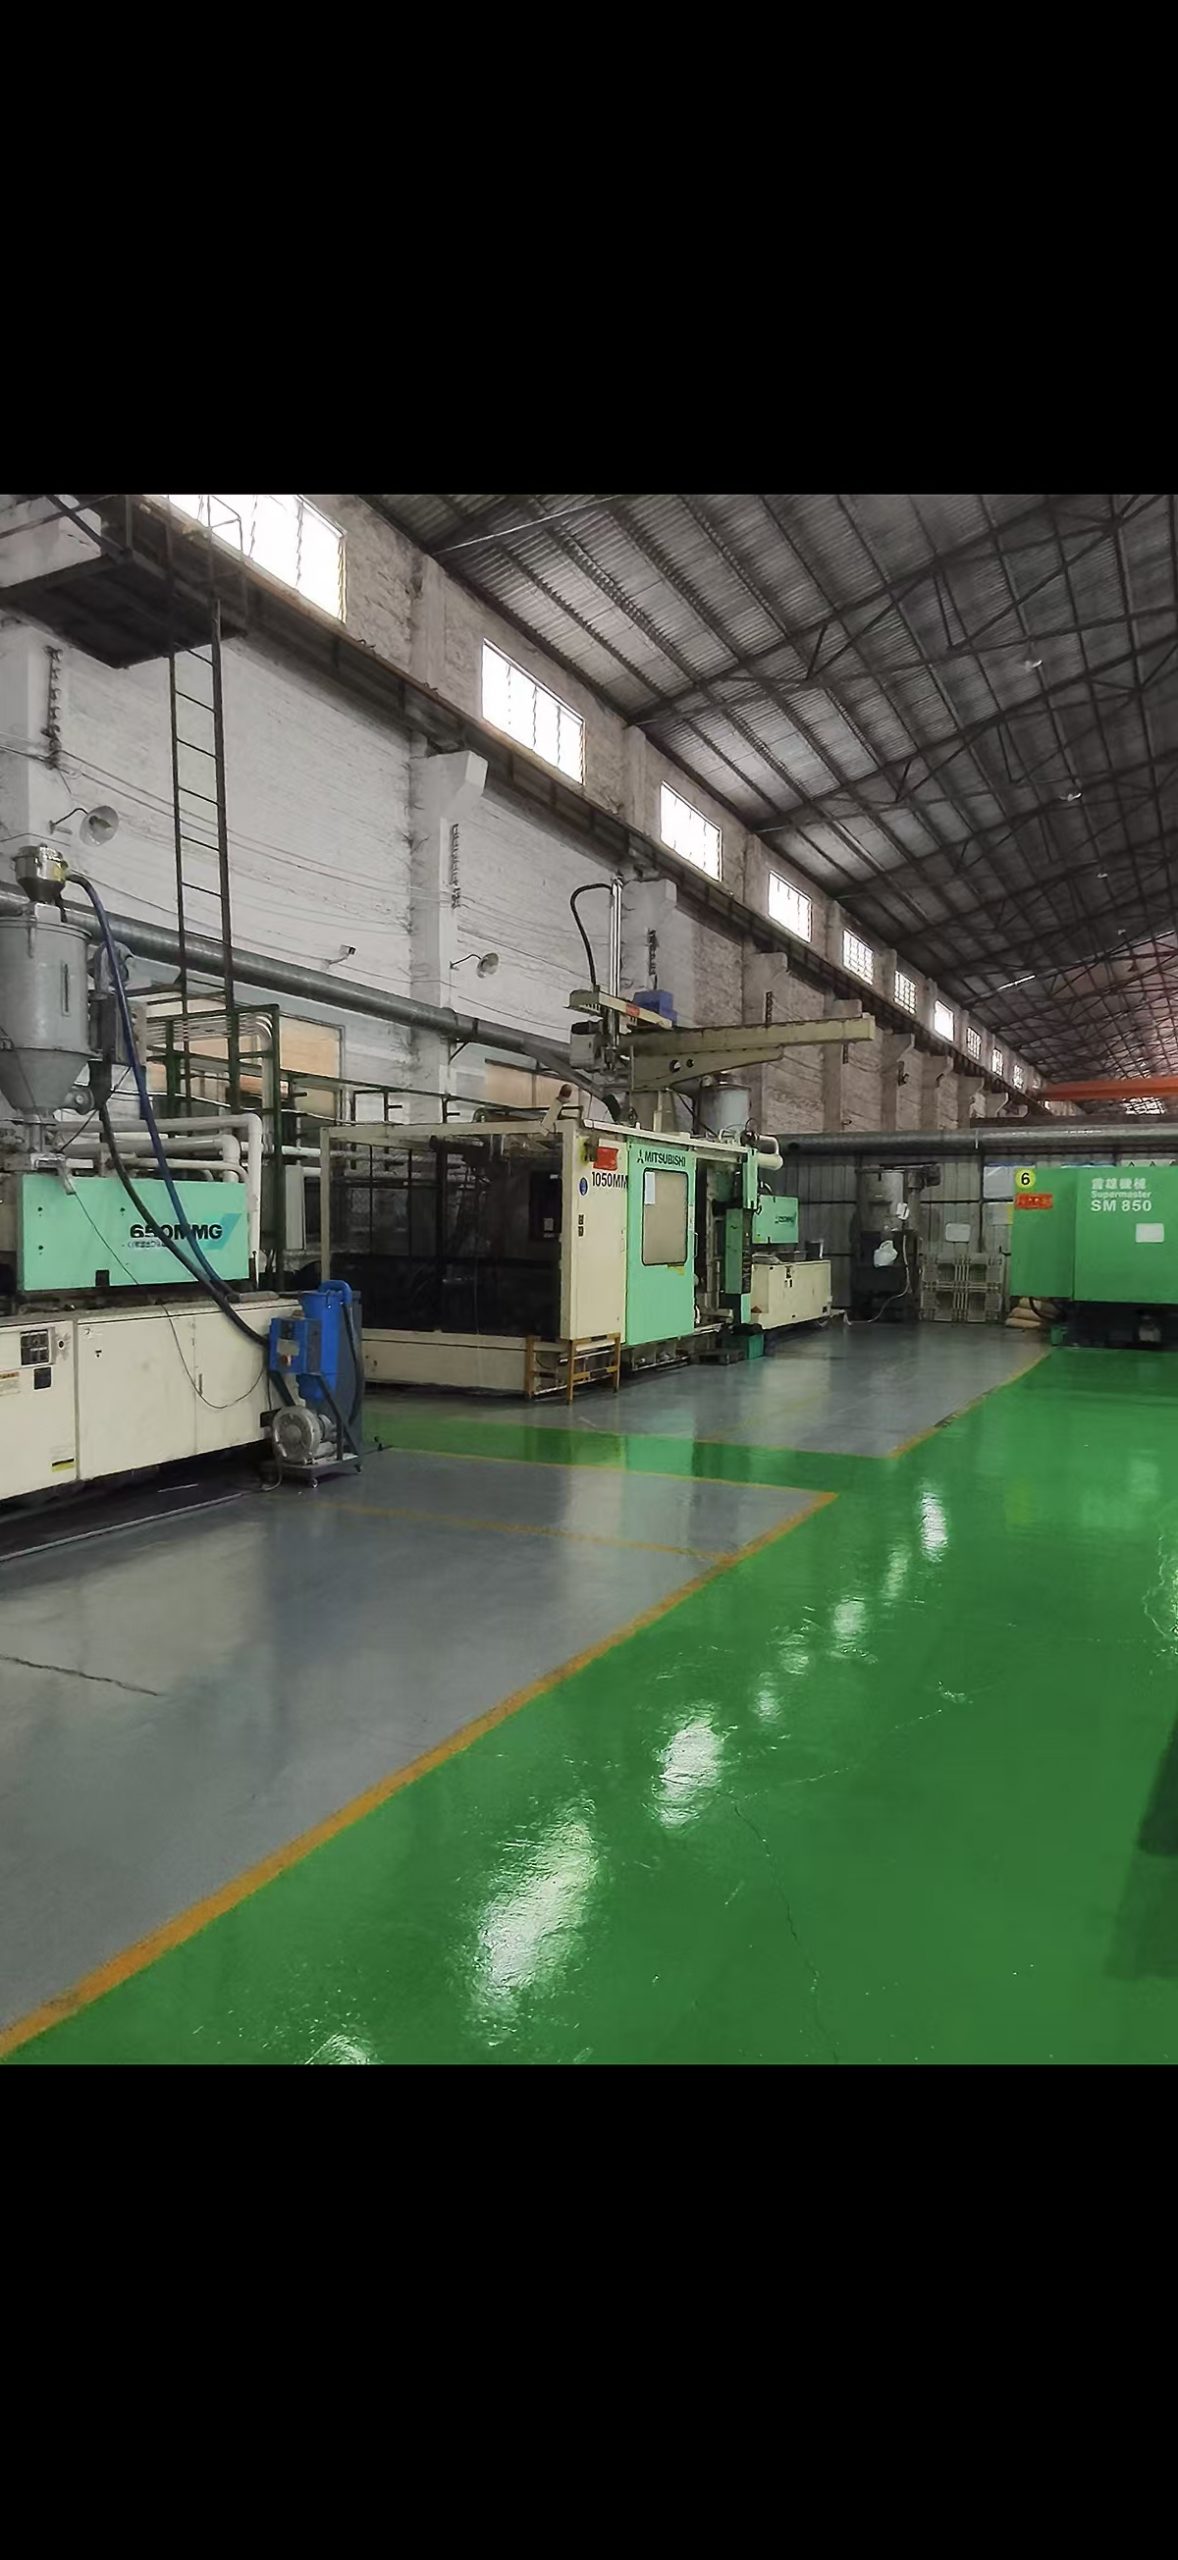
Most of the price of a moulded plastic part is bought and sold in seconds. Machine time is billed by the hour, and a cycle that runs 60 seconds versus 40 halves the output of that machine. Understanding the cycle — especially the cooling phase — tells you why parts cost what they cost, and which design changes genuinely save money.
Comparing suppliers or processes? The injection molding guide frames the key trade-offs.
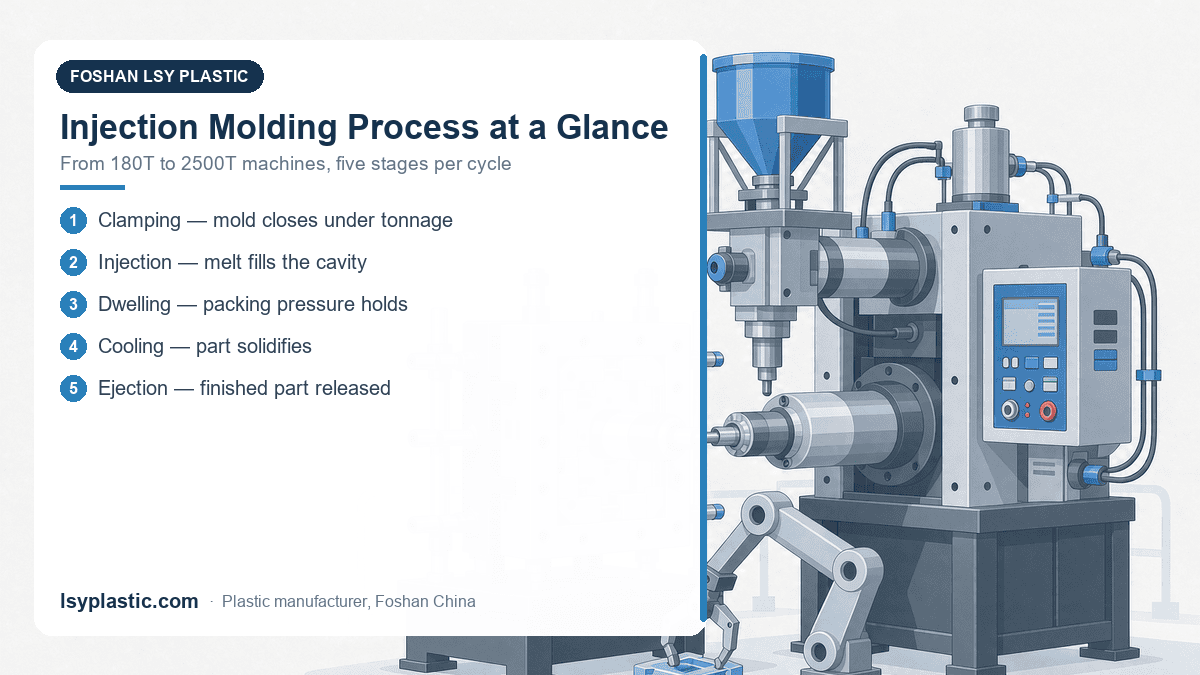
The four phases of a cycle
| Phase | What happens | Share of cycle |
|---|---|---|
| Injection | Molten resin fills the cavity | 10–20% |
| Packing/holding | Pressure compensates shrinkage | 5–10% |
| Cooling | Part solidifies in the mould | 50–70% |
| Ejection | Part removed, mould closes | 5–15% |
For a large part like a pallet or crate, total cycles run from under a minute (thin-walled small bins) to several minutes (thick structural pallets). Multiply by thousands of parts and the seconds become the price.
The square rule: thickness is destiny
Cooling time scales roughly with the square of wall thickness. Double the thickness, quadruple the cooling. This single relationship explains most of moulding economics:
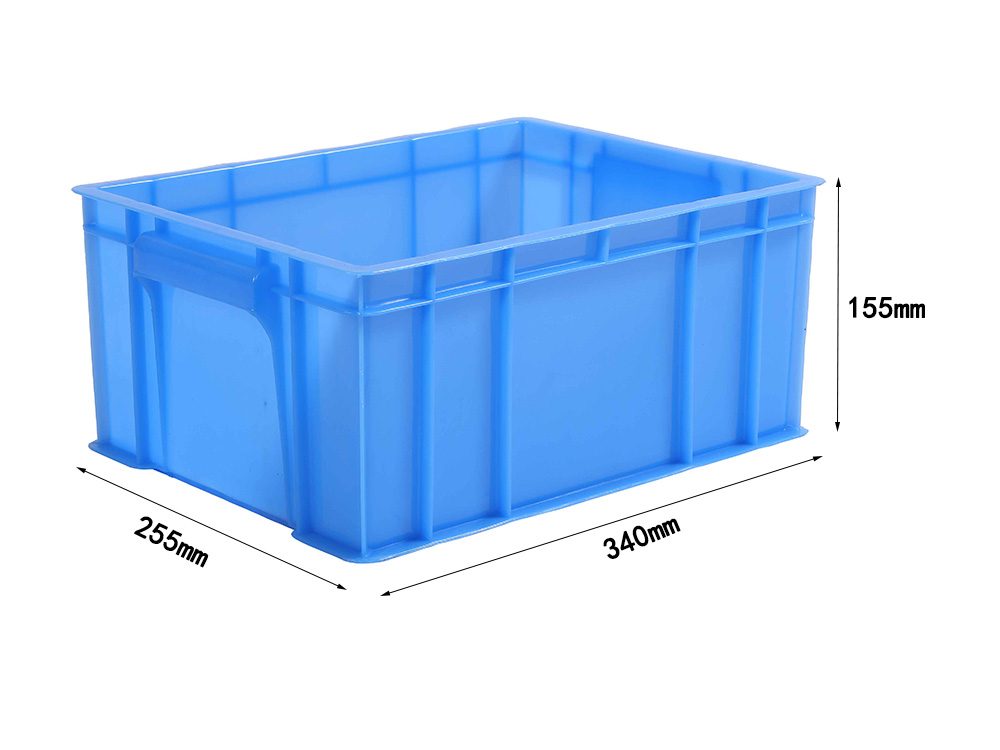
- Thin-walled crate at 3 mm → fast cycle → low machine-time cost per part
- Thick-walled bin at 6 mm → ~4× cooling → machine-time dominates material cost
- Ribbed thin wall → same stiffness as thick plain wall, fraction of the cycle
This is why structural design advice always says thin walls with ribs — the engineering is covered in our wall thickness and rib design guide. The buyer’s version: ask any supplier quoting a thick part whether a ribbed design could do the same job at lower thickness.
Other levers that shorten cycles
- Resin flow grade — faster-flowing grades fill thin walls at lower pressure and temperature, shortening both injection and cooling.
- Mould cooling design — well-placed cooling channels near thick sections remove heat faster than brute-force longer cycles. Tooling quality shows up here.
- Melt temperature discipline — running hotter than necessary lengthens cooling; running too cold lengthens injection. Experienced process setters hold the window.
- Batch consistency — interrupted short runs waste machine hours on startup scrap and re-stabilisation. Steady long runs are cheaper per part.
What shortening must never mean
There is a fraudulent way to shorten a cycle: eject the part hot and let it cool in air. The seconds saved are paid back as warping, sink marks and dimensional drift — defects that pass a quick visual check and fail in service or assembly. This connects directly to incoming quality control: our quality inspection guide covers what to check (flatness on a surface plate, dimensional sampling) so this shortcut is caught at goods-in, not in the field.
Reading a quote with cycle eyes
| Quote signal | Cycle-time interpretation |
|---|---|
| Thin-walled ribbed design proposed | Supplier is engineering cost out — good sign |
| Quote per part far below market | Check for hot-ejection shortcuts or recycled resin |
| Cavity count offered (2-cavity, 4-cavity) | More parts per cycle — real economies for small parts |
| Long tooling lead time quoted | Often pays back via better cooling channel design |
The OEM process from tooling to first article has its own timeline — see the custom injection molding OEM process guide — but the economics of every part made after tooling are decided by the cycle. Buyers who understand the square rule ask better questions and get better parts.
The Square Rule in Numbers
Cooling time scales roughly with the square of wall thickness — the single relationship that explains most of moulding economics. Written out for the wall sections a buyer actually meets:
| Wall thickness | Relative cooling time | What it means for price |
|---|---|---|
| 3 mm (thin-walled crate) | 1× baseline | Fast cycles, machine time stays a small share of part cost |
| 4.5 mm | ~2.25× | A visible cost step — worth questioning the design before accepting |
| 6 mm (thick-walled bin) | ~4× | Cooling dominates — machine time can outrun material cost |
| Ribbed 3 mm wall | Close to 1× | Same stiffness as a thick plain wall at a fraction of the cycle |
Put the two rules together: cooling is 50–70% of the cycle, and doubling thickness quadruples cooling — so doubling wall thickness pushes the total cycle up by roughly 2.5–3.3×. That is the strongest single lever on part price a buyer can question. When a quote lands on a thick part, ask for the wall thickness and the rib plan; the answer separates suppliers who engineer cost out from those who bill machine hours.